Thin Stone Veneer Over Underfloor Heating: What Actually Decides Whether It Works
Short answer: thin stone veneer and natural stone tiles generally perform well over underfloor heating because stone has low thermal resistance and transfers heat efficiently; the failure that ruins jobs is not the stone cracking from thermal shock, it is differential movement between the heated screed, the adhesive layer, the panel backing and the joints. The decision belongs to the whole floor system, not a brochure claim that “natural stone tolerates heat.” A distributor answering a tile contractor needs three things from the factory: the relevant product standards referenced for the stone (flexural strength, water absorption, thermal and moisture cycling for flooring-grade units), dimensional stability data, and an installation system written for cyclic movement, including movement joints and a deformable adhesive. Wall cladding in a heated room is a different, far simpler case than a floor panel exposed to foot traffic over a live heating circuit.
The Nordic and Alpine market has made this a standard sales objection. Buyers moving from tile distribution into natural stone cladding meet the same question on site: can the thin ledge or interlocking panel go over the wet underfloor heating loop that runs under the lobby floor? Most factories have never been asked to document the answer for a floor, because they ship the product as a wall cladding. That mismatch is where a distributor either wins the account with clear evidence or loses it to a porcelain supplier who already has a heated-floor data sheet. This article reframes the question the way a specifier asks it, and lays out the evidence a stone factory can realistically produce before a heated-floor job is approved.
The Failure Is Movement, Not a Thermometer
When a screed is heated, it expands; when the system cools overnight, it contracts. That cycle repeats daily across a heating season. Stone, adhesive, backing and screed all have different coefficients of thermal expansion and different moisture responses, and they are bonded together. If the adhesive is too rigid, if it is applied with voids instead of full coverage, or if the field is restrained at walls, thresholds and columns with no room to move, the stress concentrates and something debonds, curls or cracks. The stone is rarely the weak link in that chain; it is the visible casualty of a movement problem the design never accommodated. That is why the right mental model is cyclic movement compatibility, not maximum temperature.
This is exactly why a panel marketed for vertical cladding cannot be waved onto a floor by analogy. Thin veneer optimized for weight per container and wall bond is a different mechanical duty than a floor unit carrying traffic, point loads and the movement of a live heating circuit. The relevant European product route for flooring is the natural stone modular tile standard, EN 12057, which characterizes resistance to thermal and moisture cycling, thermal conductivity and flexural strength for floor and stair use, alongside the thermal shock method EN 14066. Passing those tells a contractor the durable stone will not degrade under cycling; it does not, by itself, certify the installation. The trade bodies that govern tile and stone flooring make the same distinction, and the guidance a distributor should hand a specifier reflects it rather than pretending a data sheet covers workmanship.
What to Tell the Contractor About the System
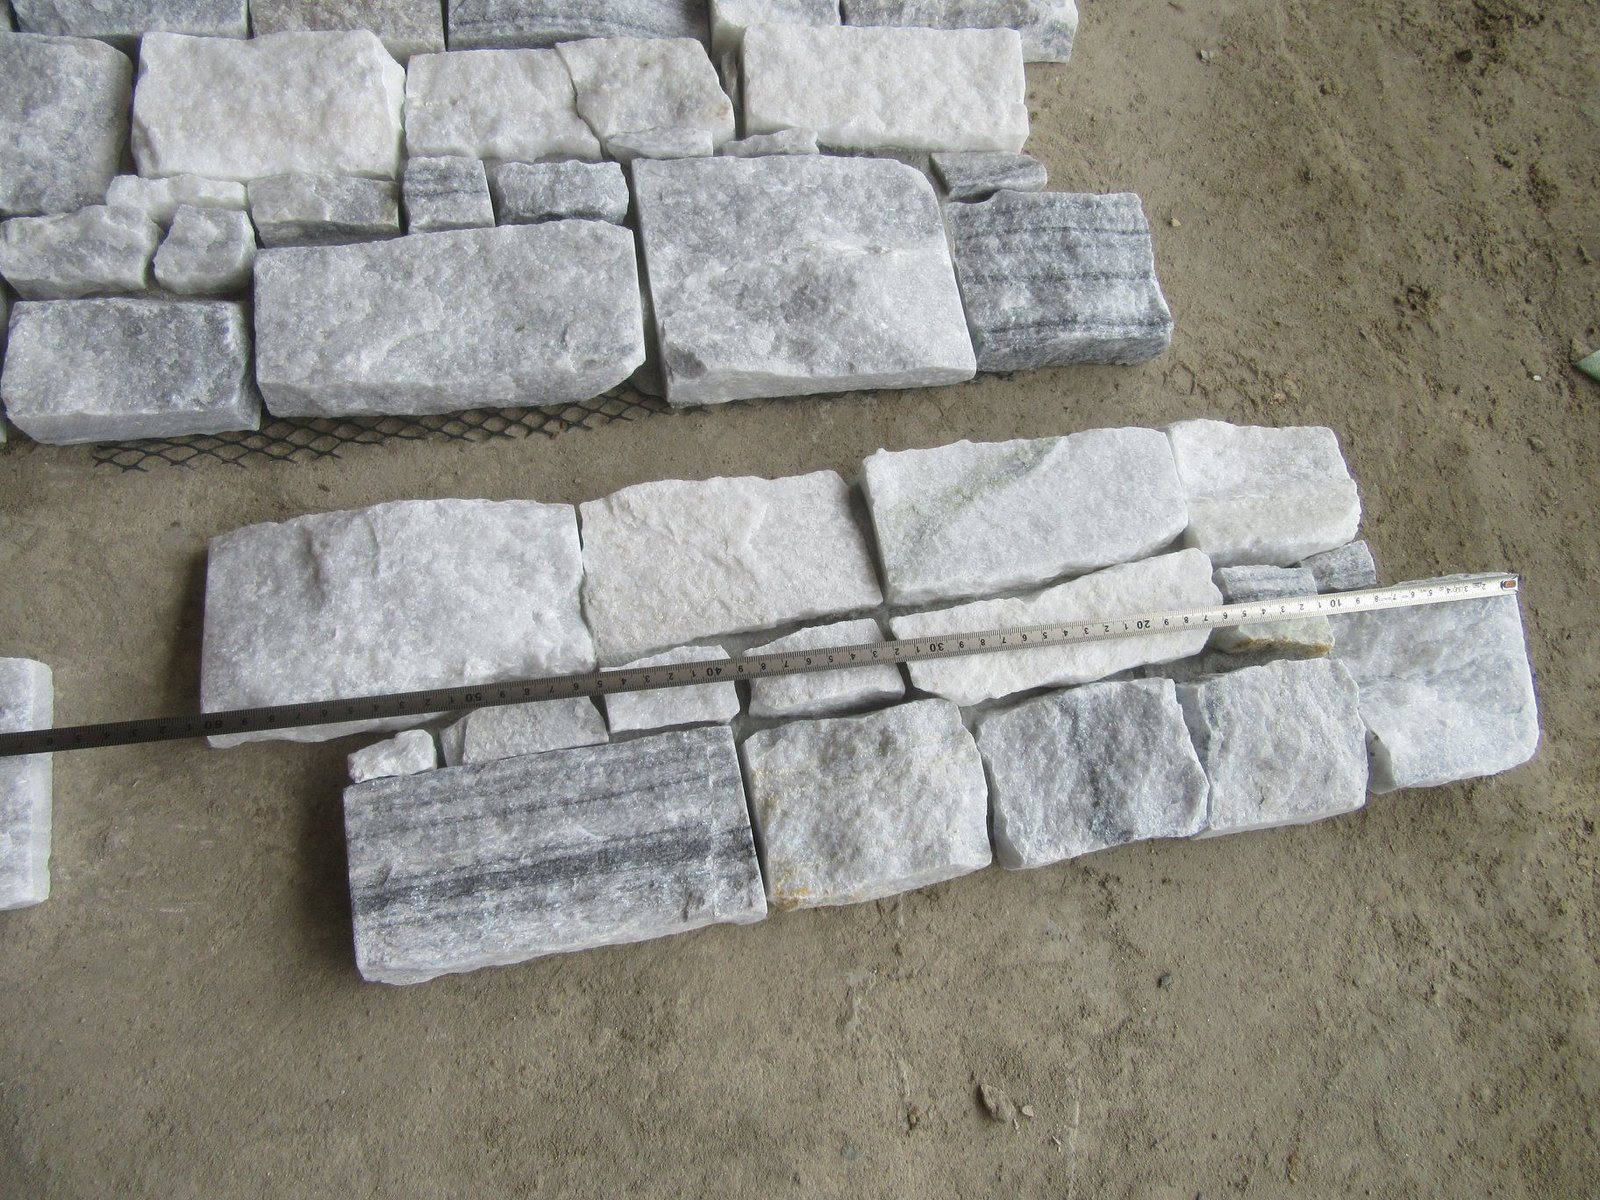
Three practical layers control the outcome. First, the screed and its joints. The structural, construction and screed joints must continue through every subsequent layer and are never bridged with adhesive, panel or grout. A heated screed that is not jointed at its perimeter, between heating zones and at thresholds will push that movement into the stone no matter how good the tile is. Second, the adhesive. A cementitious adhesive for this duty needs to be deformable enough to absorb repeated shear and tensile movement, and it needs full coverage; voids under a panel become stress risers and the most common cause of the hollow spot that later pops. European adhesive classification under EN 12004 identifies improved and deformable grades for exactly this kind of demanding substrate. Third, the panel itself, chosen for the floor duty with the standards above, dimensionally stable, and approved for the temperature and moisture exposure of the actual system.
Temperature limits belong at the bond line, not the boiler. The figure that matters is the surface and adhesive-interface temperature, which a commissioning ramp controls. Heating should be brought up gradually, the screed fully dried and cured before the panels go down, and the completed floor ramped back to operating temperature slowly rather than fired up on day one. Screed manufacturers and heating-loop suppliers publish their own maximum surface-temperature guidance for floor coverings; the stricter of that guidance and the adhesive datasheet governs the job, and a distributor’s installation note should say so instead of quoting a single number from memory. Rushing that commissioning sequence is a frequent silent cause of failures that appear weeks after the crew has left site.
When the Answer Changes: Wall Versus Floor
A distributor who treats these as one product conversation gets into trouble fast. Wall cladding installed in a room that happens to have underfloor heating is normally unaffected by the loop beneath the floor; the relevant considerations are the same as any interior cladding job, substrate prep and adhesive coverage, and the room’s general temperature cycling is mild. A floor panel sitting directly on a heated screed and carrying foot traffic, furniture and spill risk is the demanding case, and it is the one that needs the flooring-grade documentation. The same natural stone can be right for one and wrong for the other, so the first question to the contractor is which they are specifying. That single distinction protects the factory from approving a thin wall veneer for a duty it was never built for, and protects the distributor from a claim on a job that was never a wall application.
The Evidence Pack a Chinese Stone Factory Can Realistically Supply
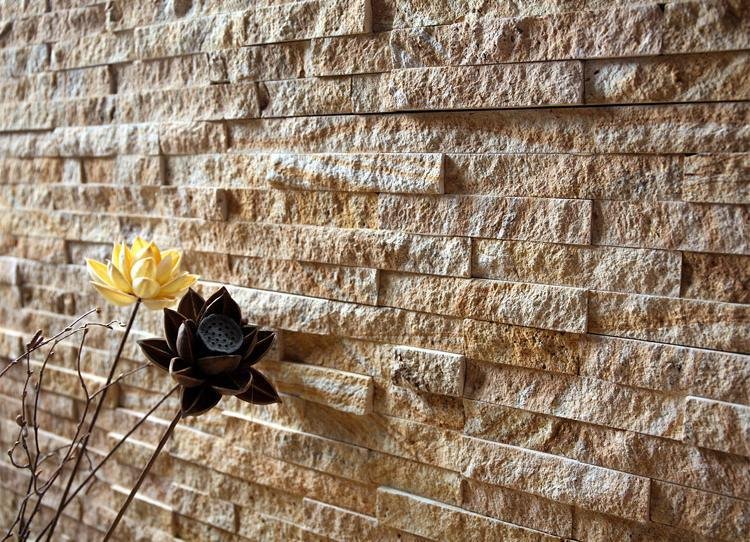
Ask for the specific, not the general. A defensible heated-floor pack contains: flexural strength of the actual stone variety, finish and thickness on the proposed product, not a generic claim, because a panel that spans one carrier or adhesive bed at one value fails at another; water absorption, the same figure that governs freeze-thaw and staining behaviour and is discussed in the site guide to water absorption in stone panels; thermal and moisture cycling results to the relevant flooring standard where a floor duty is claimed; a statement of dimensional tolerance and thickness consistency across the batch, because movement joints only work on a predictable grid; and a written installation system covering adhesive class, coverage, joint layout and commissioning ramp. The independent laboratory reports that back these figures are the same documents a specifier reads before a bid; the skill of reading a stone test report is what separates a factory that supplies methods and pass criteria from one that supplies numbers with no method. For the standards bodies behind those reports, the trade association resources and the reference to the Natural Stone Institute guidance on heated floors give the specifier a neutral place to check claims rather than trusting a sales sheet.
The honest position for a distributor is that the stone factory documents the product, the floor is designed and installed by the contractor and their screed and heating partners, and nobody in the chain signs a warranty they cannot control. A factory willing to supply flooring-grade test data and an installation note is a strong partner for these projects; a factory that only claims “natural stone is fine with heat” is a liability on a heated floor and a competitive weakness in front of a Scandinavian tile contractor who has read the standards.
Frequently Asked Questions
Can thin stone wall cladding be installed on a heated floor?
Not by default. A panel optimized as wall veneer has a different mechanical duty than a flooring unit, so it should only go on a heated floor if it is tested and documented for floor use against the relevant flooring standards, with an installation system designed for cyclic movement. Absent that, it is a wall product.
Does the sealer or backing change the heated-floor story?
Yes. A resin or cement backing forms a composite of stone, backing and adhesive with three different moisture and thermal responses, and it can change both movement behaviour and the adhesive choice. The backing is part of the system, so declare what it is and build the installation note around it, not just the stone.
What is the single most common heated-floor stone failure?
Bridged or missing movement joints and inadequate adhesive coverage, not the stone overheating. The screed expands, the restrained field concentrates stress, and rigid or voided adhesive debonds. Correct jointing and full-coverage deformable adhesive prevent most of it.